Why the 45 XP is the reference
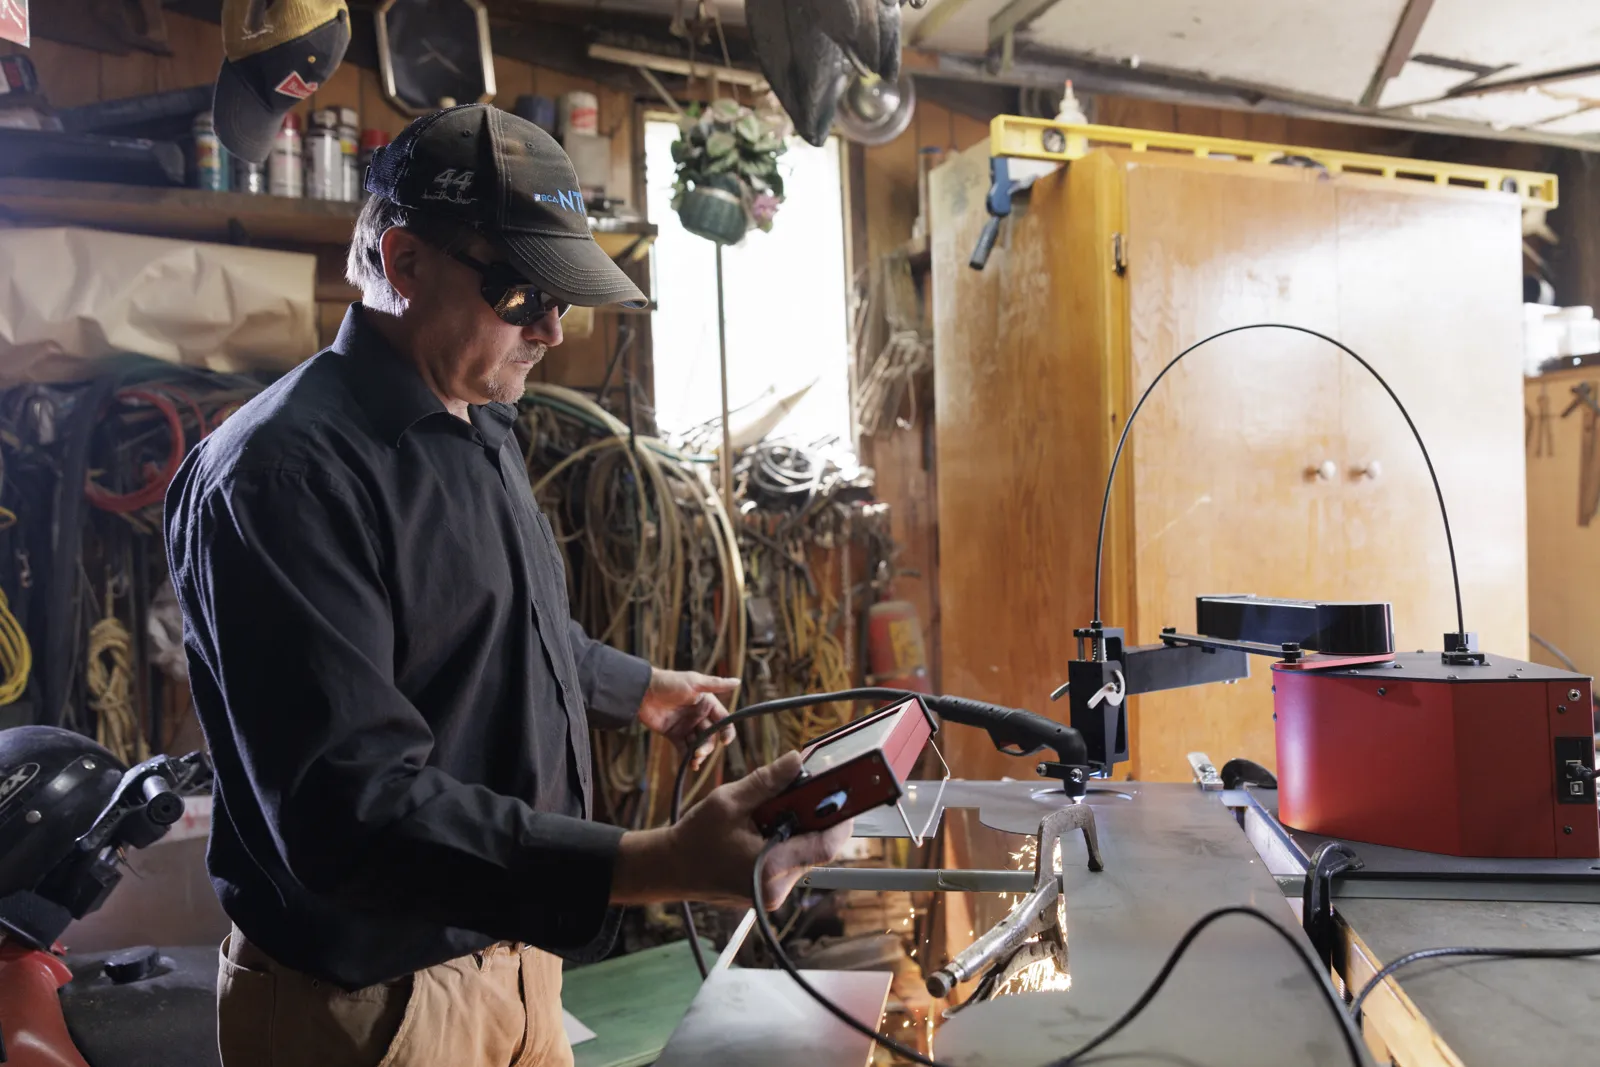
It is the cutter found in the largest number of workshops, for good reasons: 45 A, 12 mm of steel in clean cut, 16 mm maximum, 25 mm severance; a start without high frequency; consumables available from every welding supplier; and, as standard, a machine output — the CPC port — that provides everything a CNC needs. It comes in 230 V single-phase (plan a 32 A circuit for full power) and 400 V three-phase. A 45 XP bought for hand cutting becomes a CNC source without changing anything but the cable.
The CPC port: what comes out of the cutter
At the back, a round 14-pin connector. Three pairs matter to us: the start (the machine closes a contact, the arc fires), the arc transfer (the cutter signals that the arc has reached the sheet — the machine can start moving) and the divided arc voltage, an image of the cutting voltage brought down to a few volts by the cutter's internal divider. On the Powermax 45 XP, 65, 85 and 105, these are pins 3–4 for the start, 12–14 for the transfer and 5–6 for the divided voltage. Always check the manual of your version: it is one page, and it saves a burnt cable.
The cable
The shortest route: a ready-made cable. The Hypertherm cable for ArcDroid (€52) plugs into the CPC port on one side and into the controller on the other, with no soldering or setting. If you wire your own for another machine, use the original 14-pin CPC plug, a shielded cable, and connect only the useful pairs; shield grounded at one end only. Keep the cable away from the air hoses and the torch lead, and never let it lie in the sparks.
Divided arc voltage and torch height control
During the cut, the arc voltage depends directly on the distance between the nozzle and the sheet: the torch rises, the voltage rises; it drops, the voltage drops. Torch height control (THC) reads this voltage and corrects the height continuously — this is what allows cutting a warped sheet or a salvaged part without the nozzle catching. The 45 XP has a built-in divider set by DIP switches, delivered at 50:1: leave that setting, it is what the ArcDroid cable and calibration expect. During the cut, with healthy consumables, the reading is stable; if it jumps, it is almost always a worn nozzle or wet air.
Torch, consumables, air
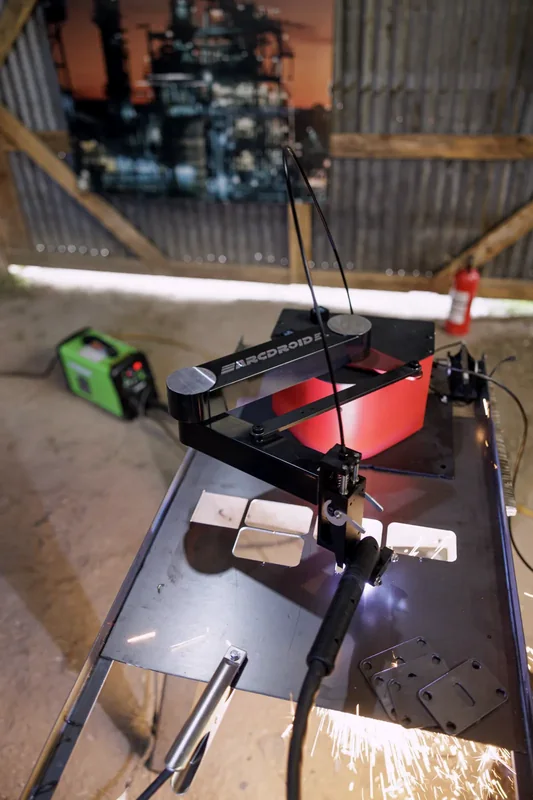
The 45 XP's Duramax hand torch fits as is in the ArcDroid's universal holder; the machine torch is not required, it remains possible. Use the 45 A shielded consumables: they tolerate accidental contact with the sheet and live longer than bare nozzles. On the air side, the 45 XP asks for about 190 l/min at 6 bar at the inlet, in dry air: a 100 l compressor with a filter-dryer on the outlet does the job; a coalescing filter just before the cutter protects the consumables from the compressor's oil and water.
Settings and first cuts
Set the cutter to 45 A, in continuous cutting mode, not grate mode. On the machine, start from the Hypertherm cut chart for the speed: from several metres per minute in 3 mm to less than a metre per minute in 12 mm. Piercing is done higher than cutting (about twice the cut height) with a delay that grows with thickness — a few tenths of a second in 6 mm, around one second in 12 mm. Then three 30 mm squares in an offcut: too slow, the dross sticks and the edge turns blue; too fast, the bottom of the cut is not pierced through. The right speed leaves a fine dross that falls off with a finger.
The mistakes that cost a nozzle
They are always the same.
- An HF-start cutter connected to a CNC: never — the 45 XP has none, one of its strengths
- The CPC port not enabled on some models (machine torch or jumper, procedure in the Hypertherm manual)
- Two pins swapped on a home-made cable: the cutter fires non-stop or never fires
- Wet air: unstable arc, consumables lasting a third as long, a voltage reading that jumps
- Worn consumables kept "to finish the part": the THC dives, the nozzle touches, the part is redone